Presses, hand welders, spin and metal welding systems — with the joint design, materials and troubleshooting knowledge that decides whether any of it works.


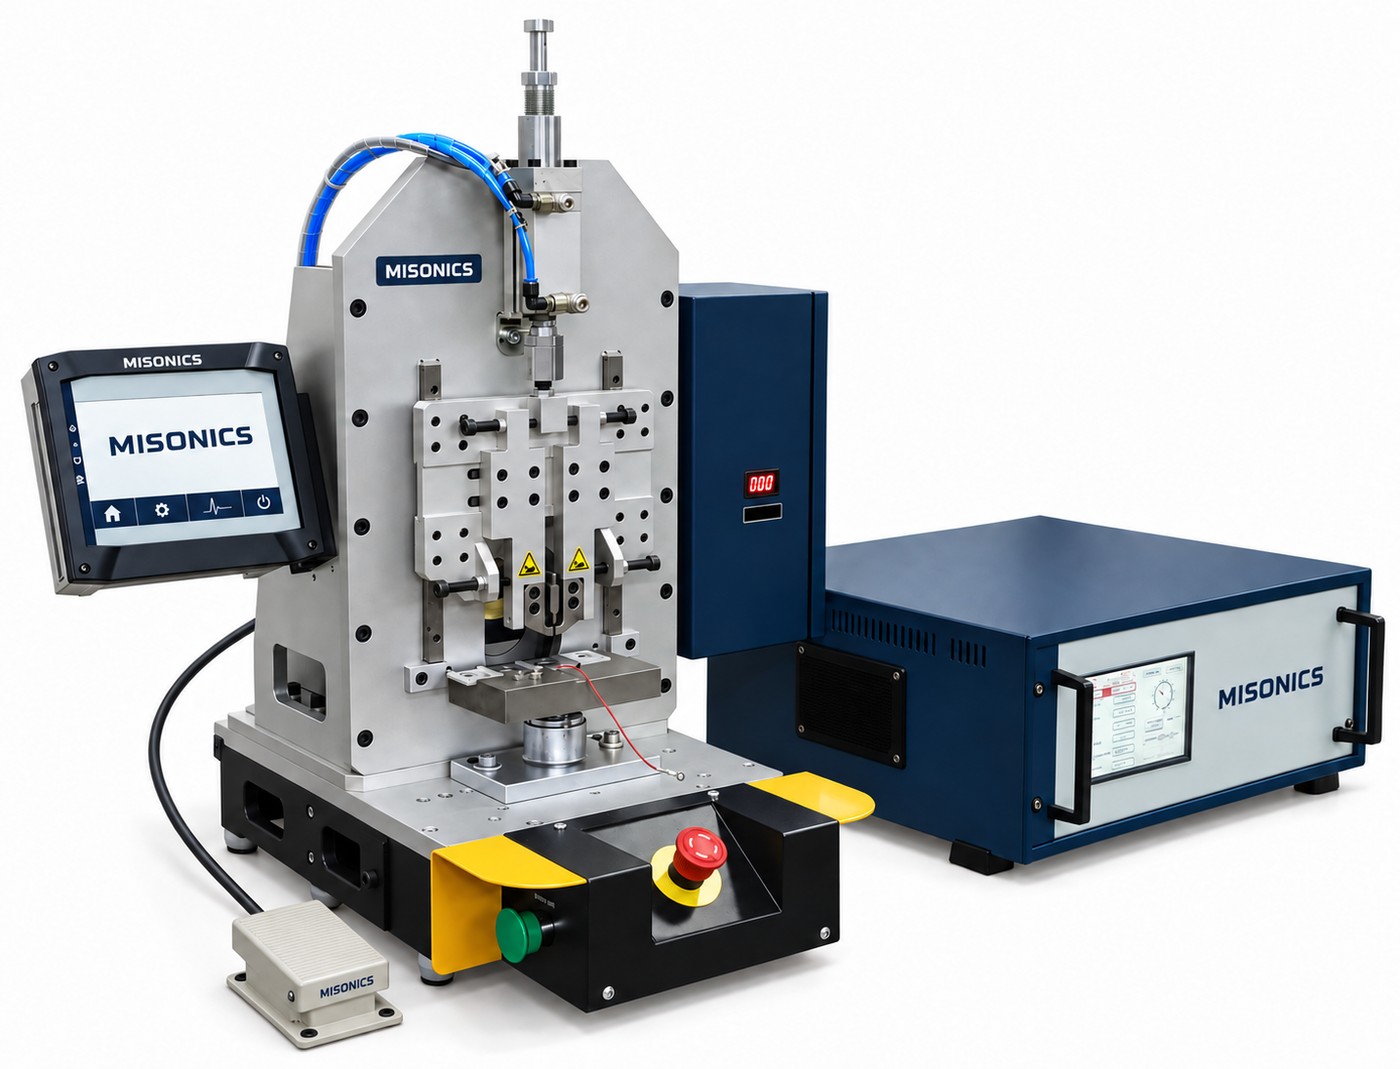
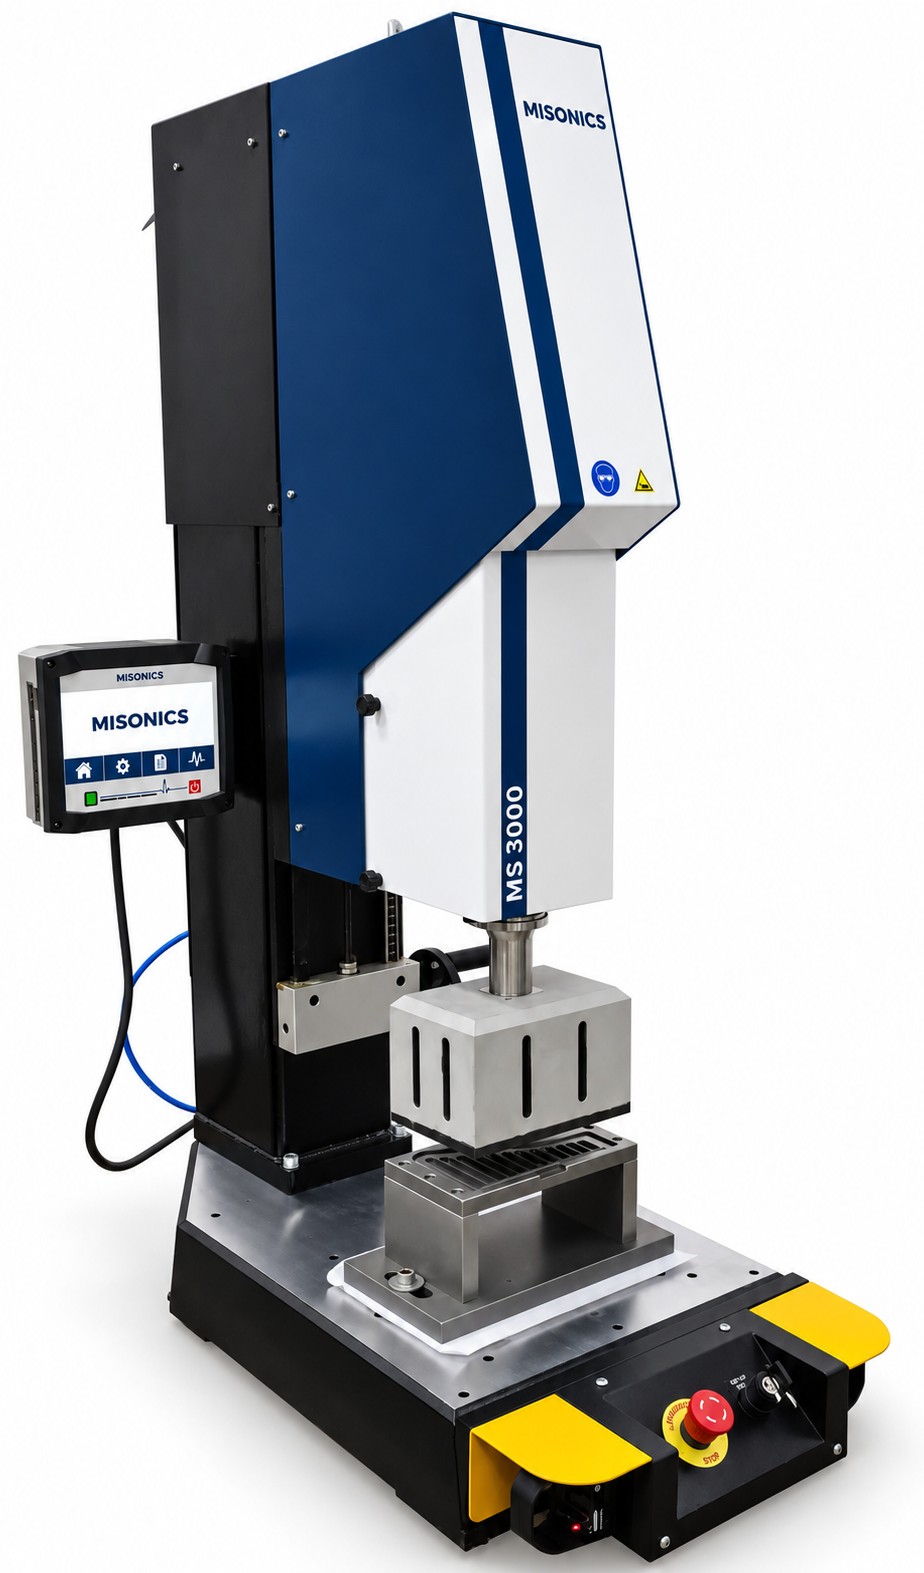
MS 3000, set up for a job. The fixture holds the part, the horn comes down onto it, and the same settings run again tomorrow. Tooling is made to the part — it is not something you buy off a shelf.
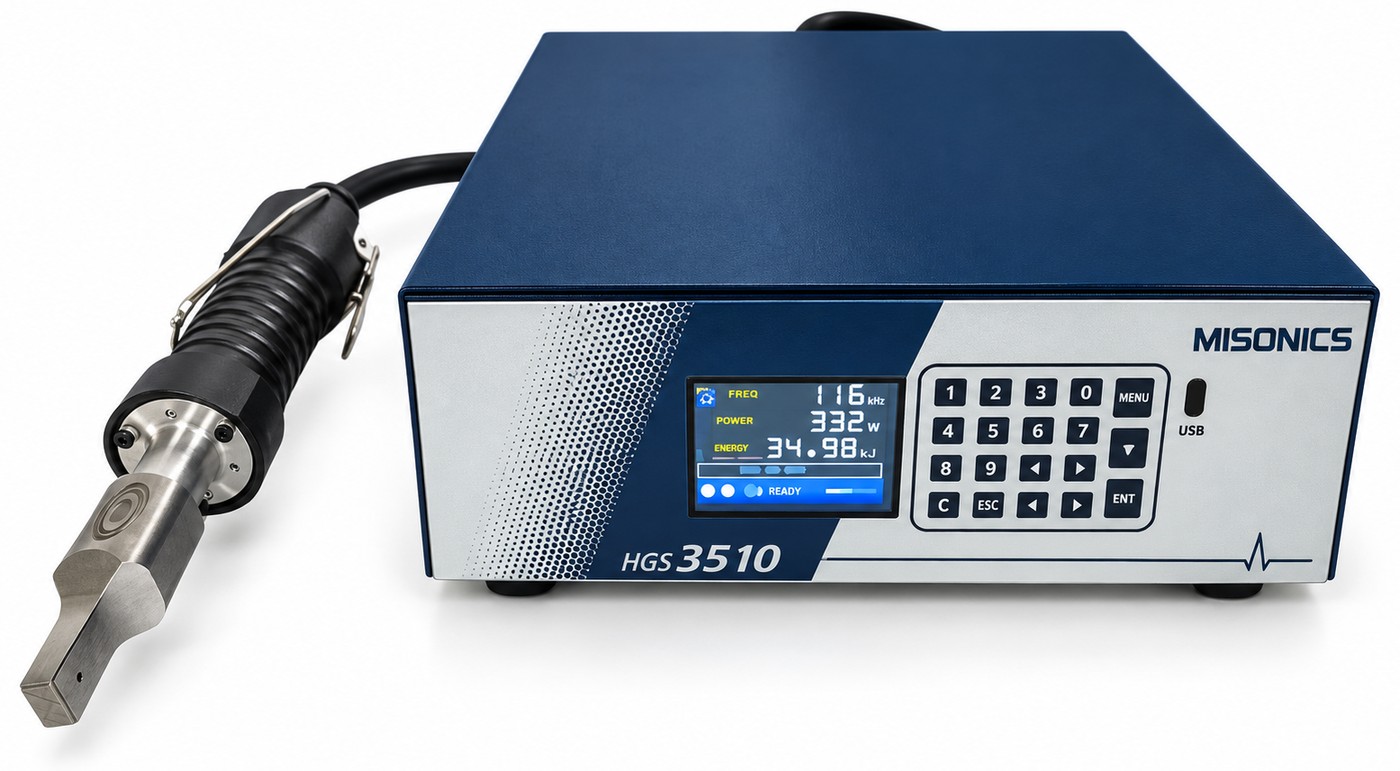
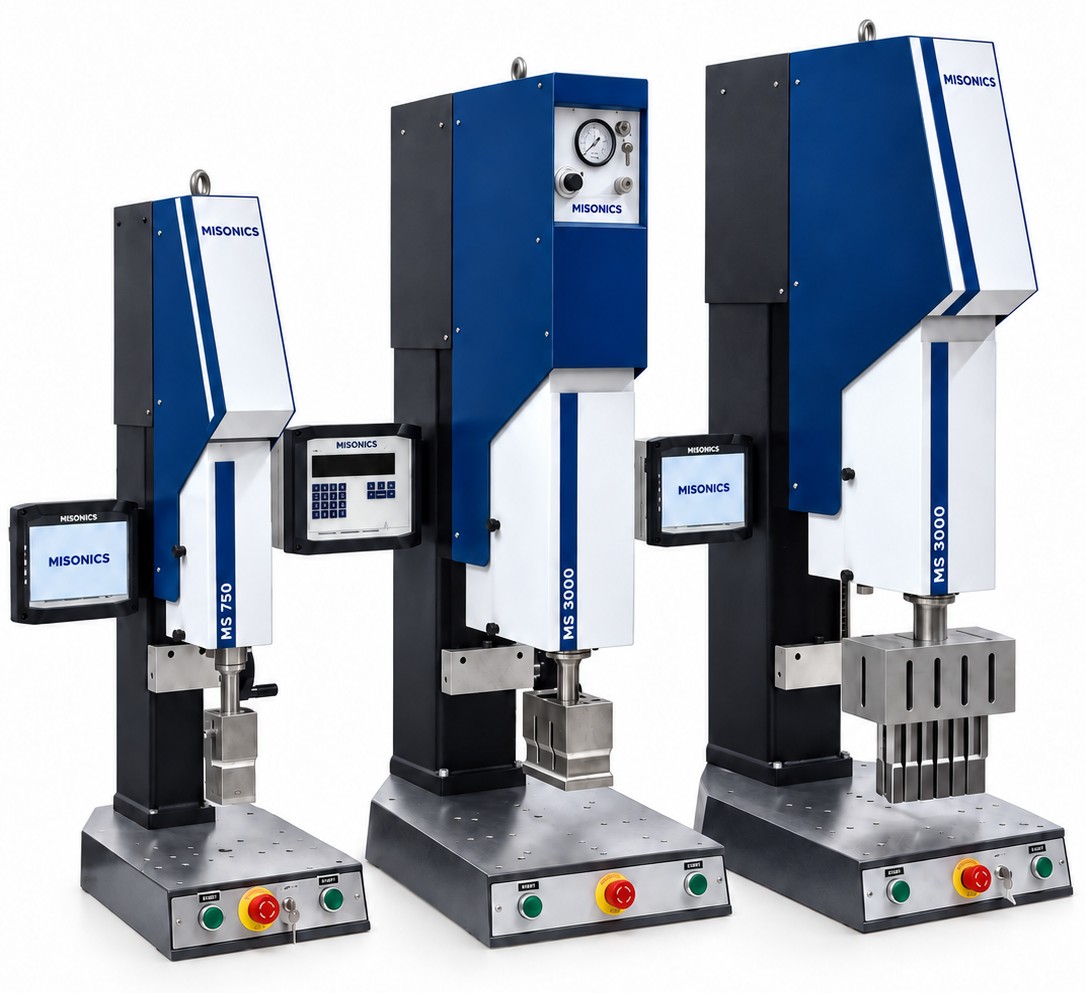
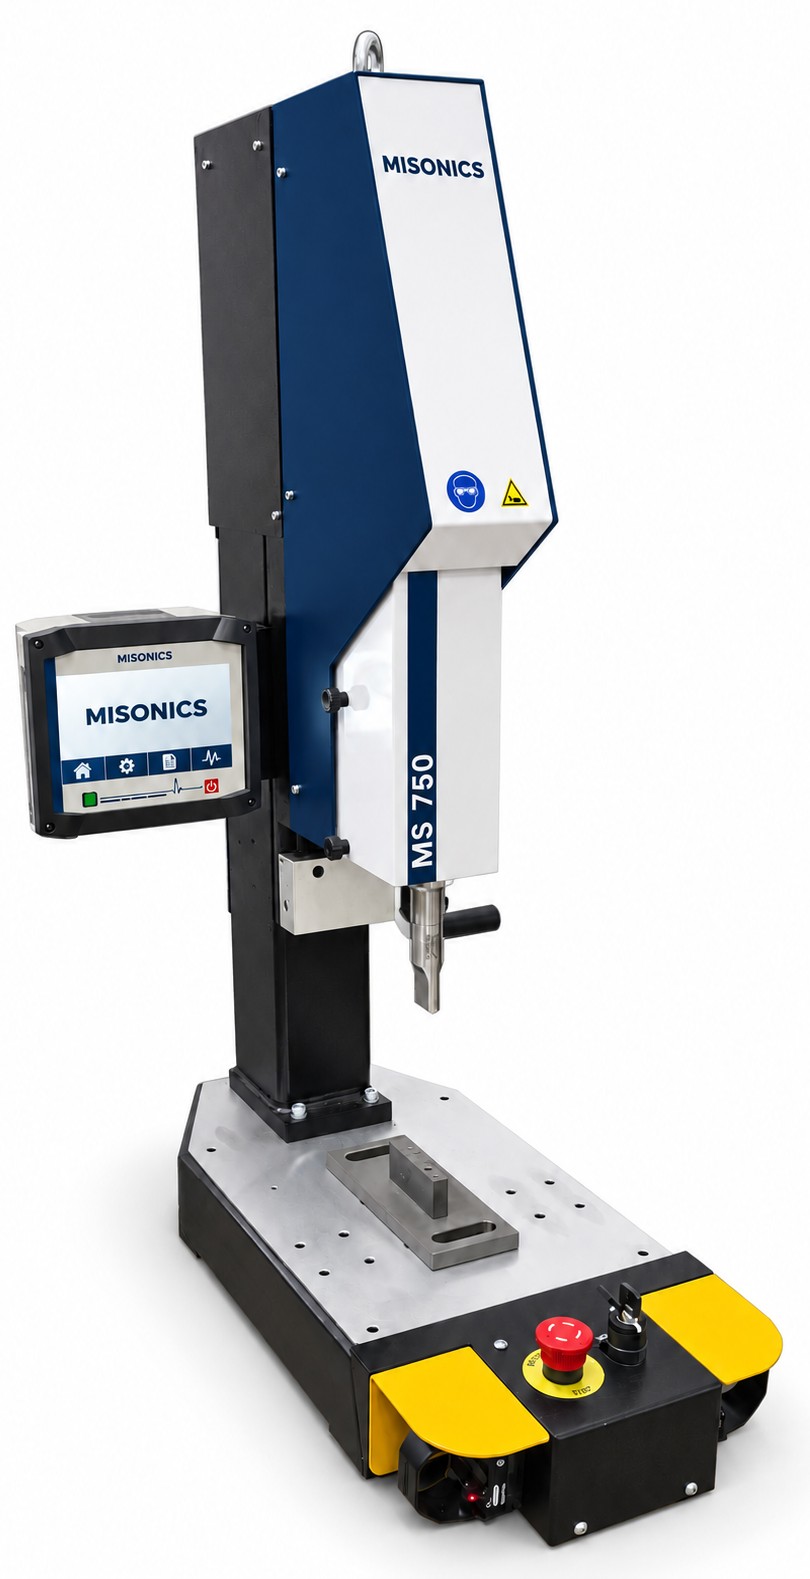
Every press on this page is the same machine underneath — a generator, a converter, a booster and a horn, driven down onto a part held in a fixture. What changes up the range is the force available, the stroke, and how tightly the weld is controlled.
The touchscreen sets amplitude, pressure and time, stores the settings per part, and logs what each weld actually did. That log is what gets you through an audit.
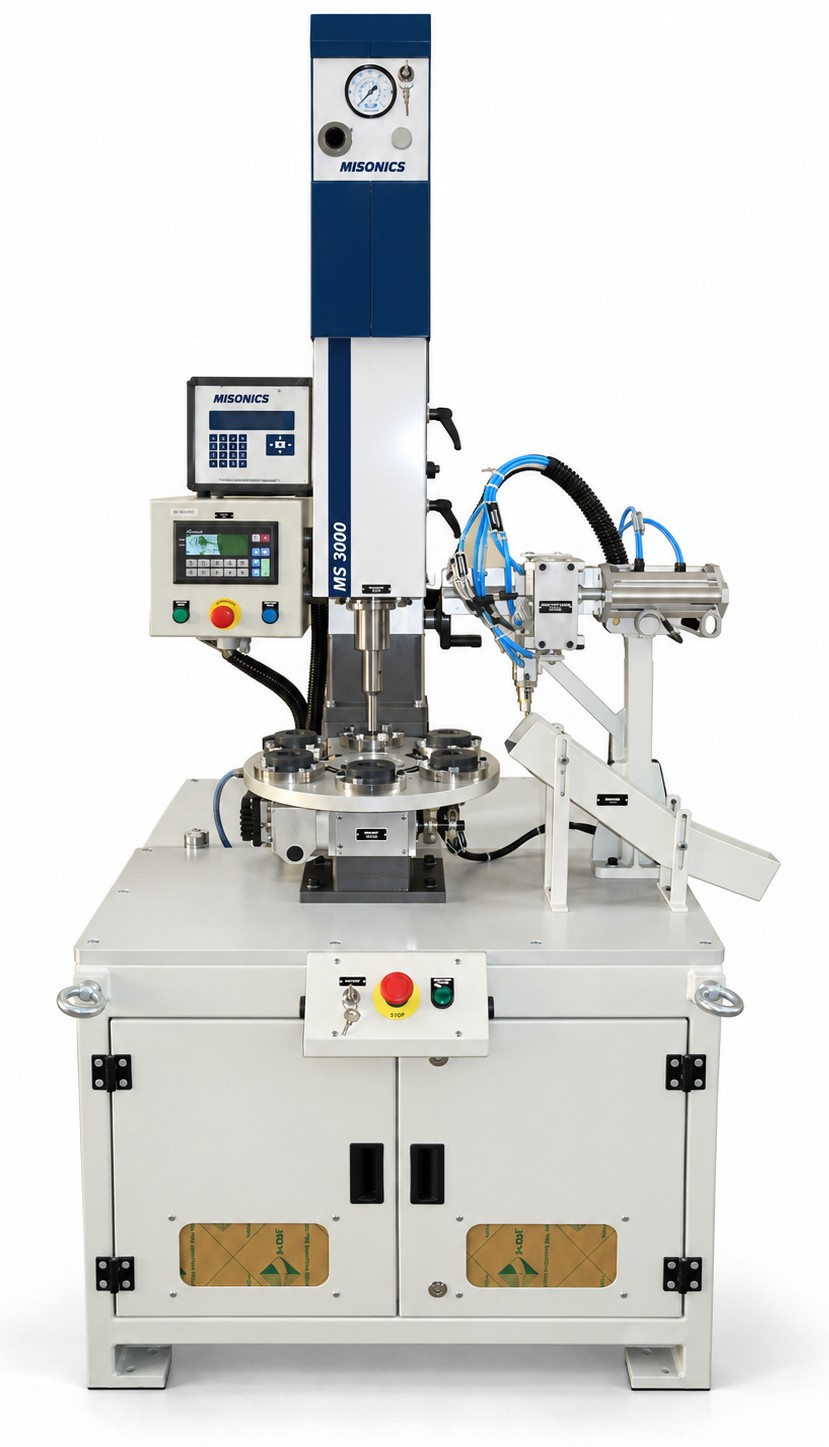
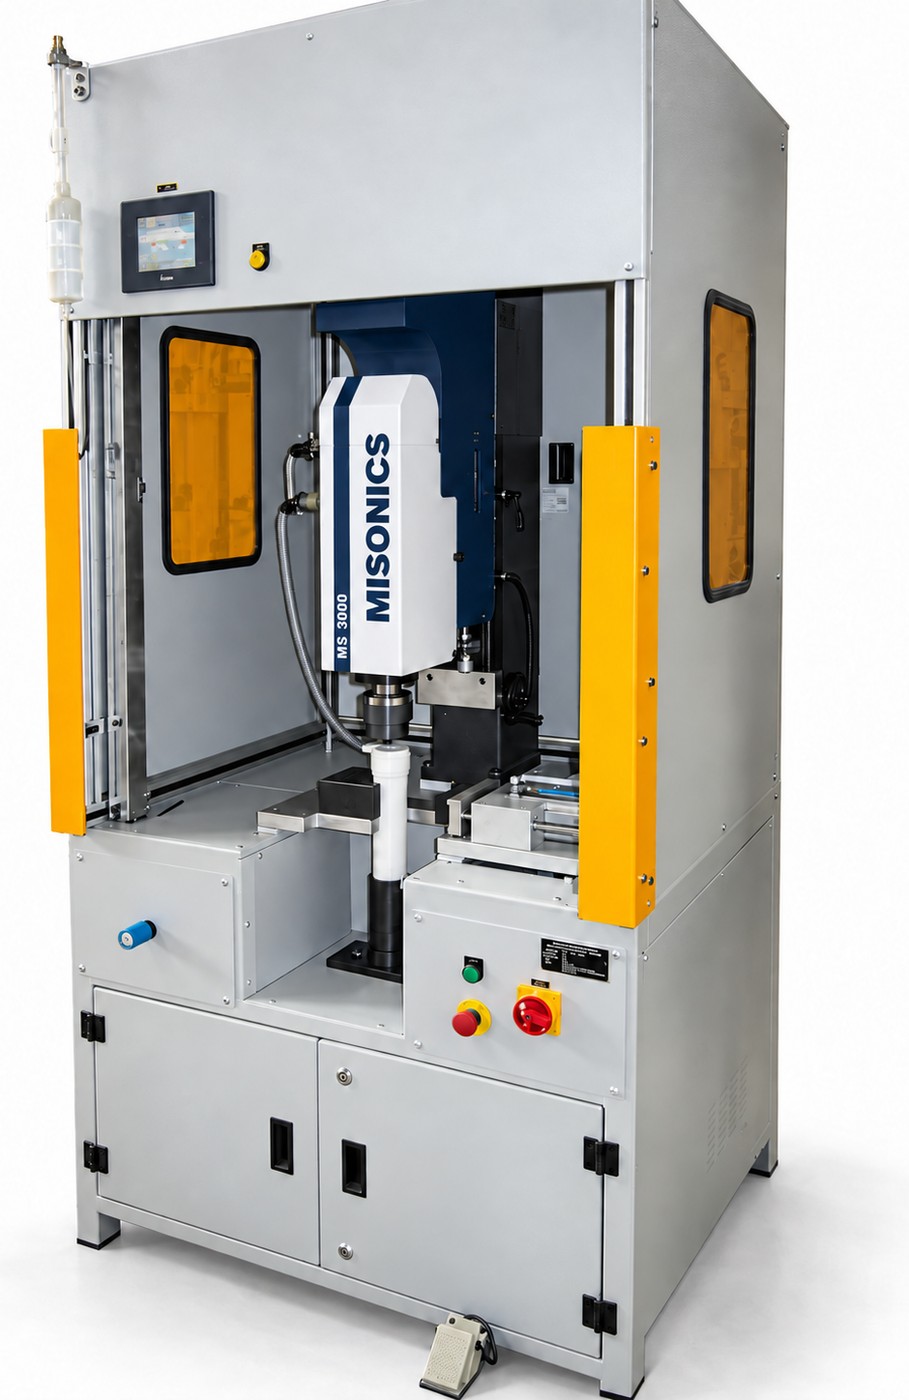
This is an MS 3000 — the same press from the bench — sitting over a rotary indexing table. Six fixtures on the dial, a pneumatic arm that feeds the part in, guarding around the work, and the generator in the cabinet underneath.
The operator loads one station while the head welds another, so the weld time stops being the bottleneck. A PLC screen sits beside the welder control: the welder owns amplitude, pressure and time, the PLC owns the index, the feed and the interlocks.
What gets engineered to the job is the dial, the fixtures and the handling. The welding head does not change.
Ultrasonic welding converts mains electricity into high-frequency mechanical vibration, drives it through one part into the joint, and uses the friction at that interface to melt and fuse the material. The weld takes a fraction of a second, adds no consumable, and leaves a joint as strong as the parent material when the joint is designed properly.
Four of those five are catalogue items. The fifth — the sonotrode — is made for your part, and it is the one that decides whether the process works. That is why a welding enquiry starts with the part, not the machine.
No adhesive, no solvent, no screws, no inserts. The cost per joint after the tooling is electricity.
Typical weld times are 0.2 to 1.0 seconds. Cycle time is usually set by handling, not by the weld.
The right joint design gives a genuine airtight, watertight seal — which adhesive rarely does repeatably.
Weld by time, energy, distance or absolute distance, with the result recorded per cycle. That is a process you can validate.
No fumes, no VOCs, no cure time, no shelf life. Matters in medical, food and electronics.
The same process runs on a bench press for prototypes and in a fully automated line at millions of parts a year.

Bench and floor-standing presses from a 54 mm hand-held head to a 6,000 N floor press. Time, energy, distance and absolute-distance weld control.

Portable welding, riveting, staking and spot welding where the part cannot come to a press — large assemblies, trim, and repair work.

Friction welding for circular joints — filter bowls, caps, reservoirs and any round part where a continuous hermetic seal is needed.

Copper and aluminium joined without heat or current — wire splices, terminals, battery tabs, busbars and tube sealing.

The stack on its own — generators, converters, boosters and custom sonotrodes to retrofit or rebuild an existing machine.
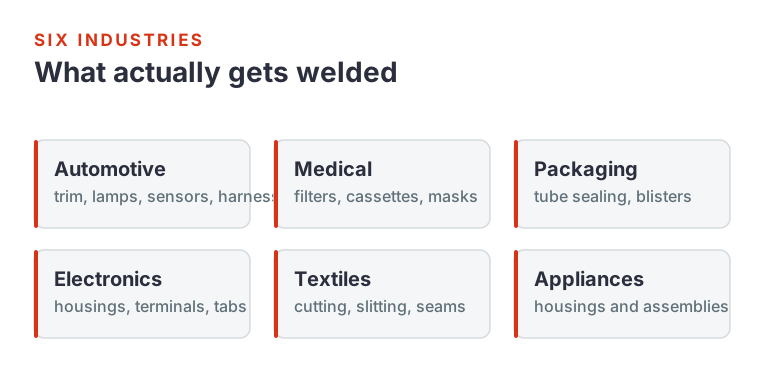
What actually gets welded: automotive, medical, packaging, electronics, textiles and appliances — and which process suits each.
Most failed ultrasonic welding projects fail in the part design, not the machine. These three cover what decides success before a purchase order exists.
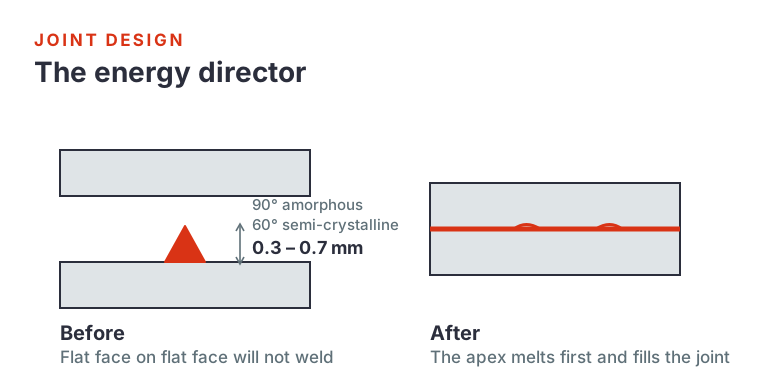
Get this right and the weld is easy. Energy director dimensions, shear joints, near-field vs far-field, and the mistakes that cannot be fixed on the machine.
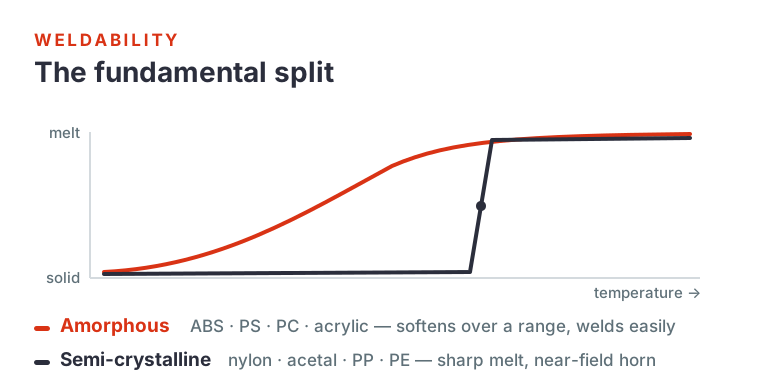
Amorphous against semi-crystalline, filler and regrind limits, moisture, mould release, and why you generally cannot weld two different resins.
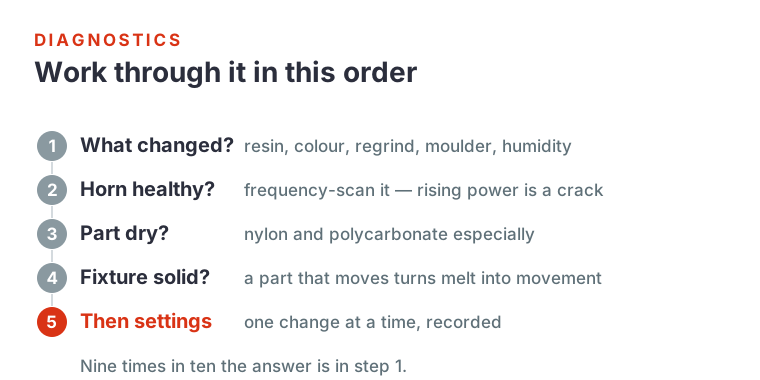
Flash, marking, weak welds, diaphragming, damaged internals and inconsistent results — causes and what to change.
Practically, that means the enquiry form asks for more than most. Resin and grade, wall thickness, joint type, what the weld has to achieve, volumes — and photos or drawings of both halves. Send that and the first reply is useful. Send “how much is a welder” and it will not be.
Ultrasonic welding is decided by the parts — the resin, the wall, the joint and what the weld has to do. Send photos and drawings through the enquiry form and you get an engineered answer.