A fouled cooler is an efficiency tax the plant pays every hour: radiators, air-to-oil coolers and shell-and-tube exchangers lose capacity to scale outside and oil sludge inside, and rodding or acid-boiling shortens their lives. This study documents the immersion recovery process for high-efficiency copper-tube coolers (Mesabi-class) and marine finned-tube exchangers.
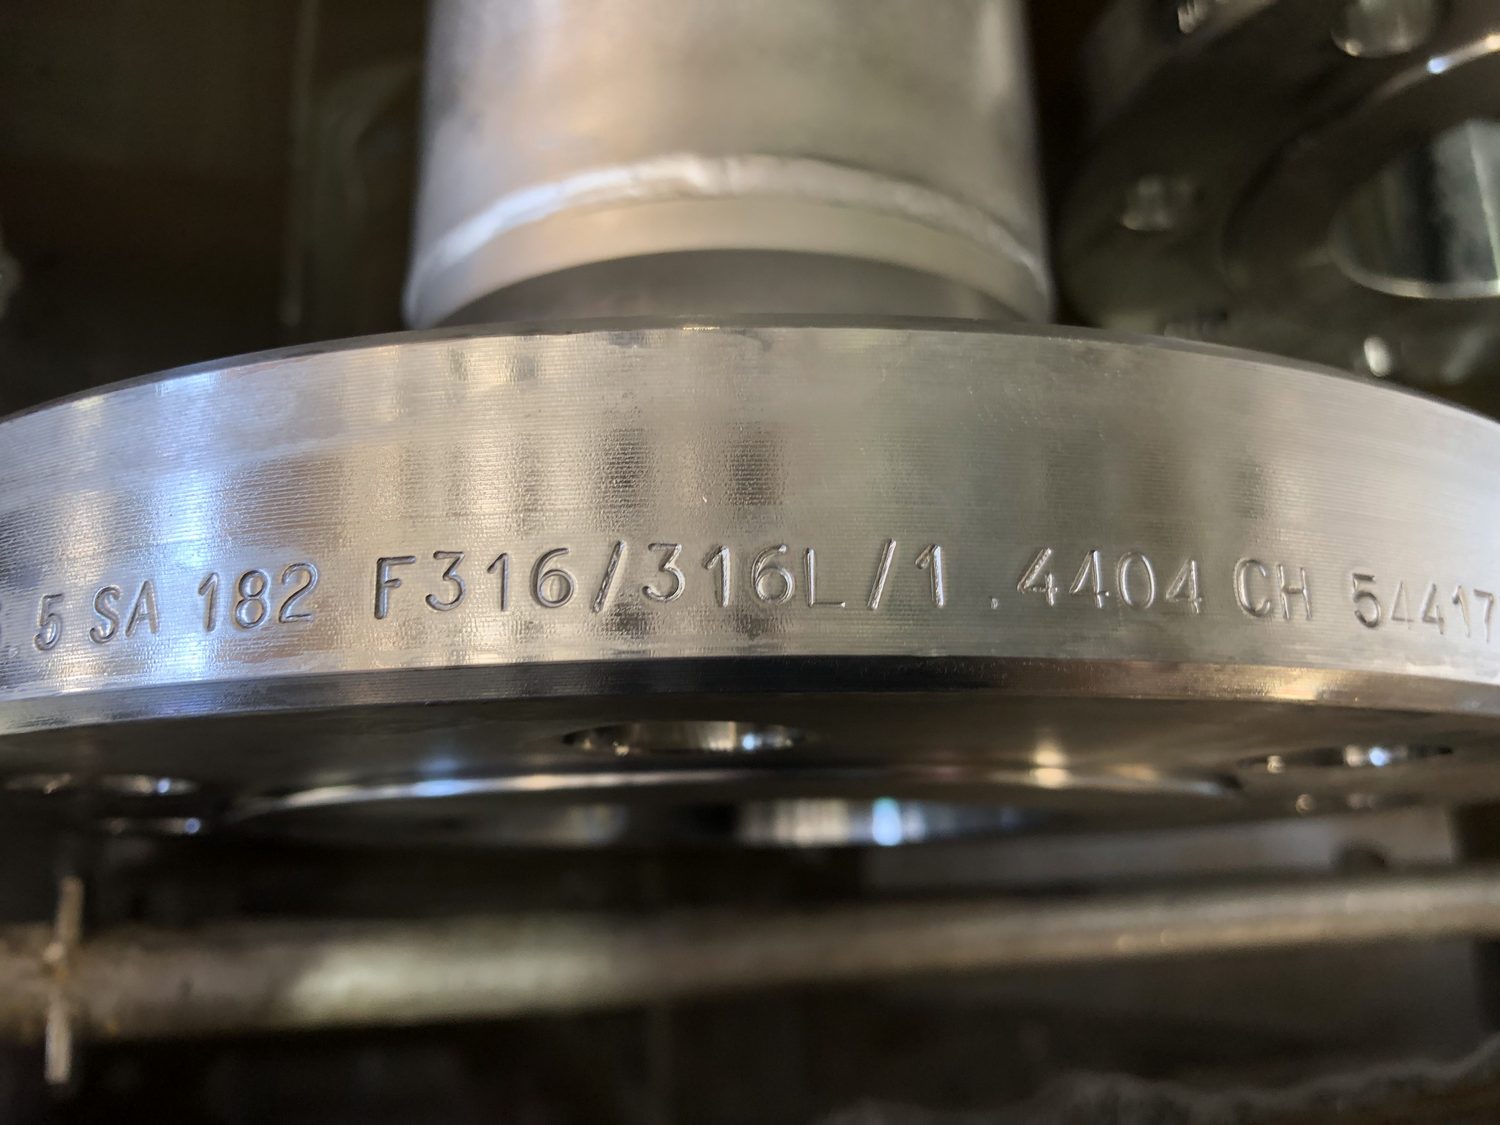
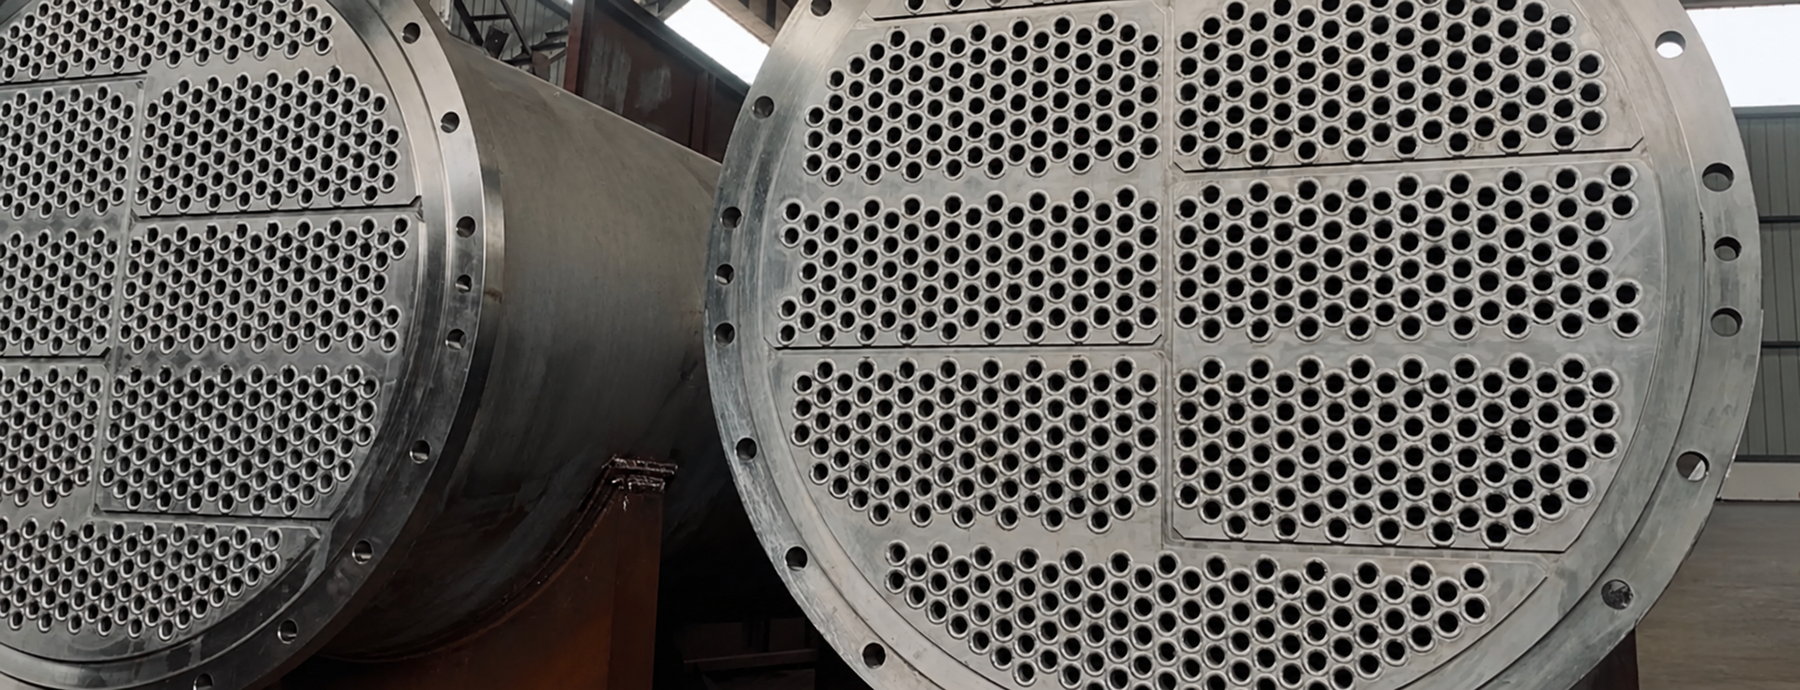 Tube sheet — every tube open after the cycle, without roddingMaterial is read off the flange stamp before any chemistry is chosenOil sludge and fouling outside, waterside scale inside — two stages
The contamination
Fin-side fouling
Dust, oil mist and organic debris matted between fins — pressure washing bends the fins it reaches and misses the core depth entirely.
Tube-side oil sludge
Oxidised oil and carbon lining air-to-oil cooler tubes — the film that turns a cooler into a heater. Degreasing chemistry, cavitation-driven, from the inside.
Waterside scale
Carbonate and silica on marine and plant exchangers — inhibited descaling territory, with the inhibitor mattering as much as the acid on thin-wall tube.
The process
| Parameter | Value |
|---|---|
| Chemistry | CoreKleen HX degrease + Descale stage where scaled |
| Temperature / cycle | Established per application |
| Equipment | Industrial tank sized to core; 360° rod retrofit for bundle vessels |
| Verification | Flow or pressure test vs baseline |
| Materials care | Inhibited chemistry on copper, CuNi and aluminium — no rodding, no fin damage |
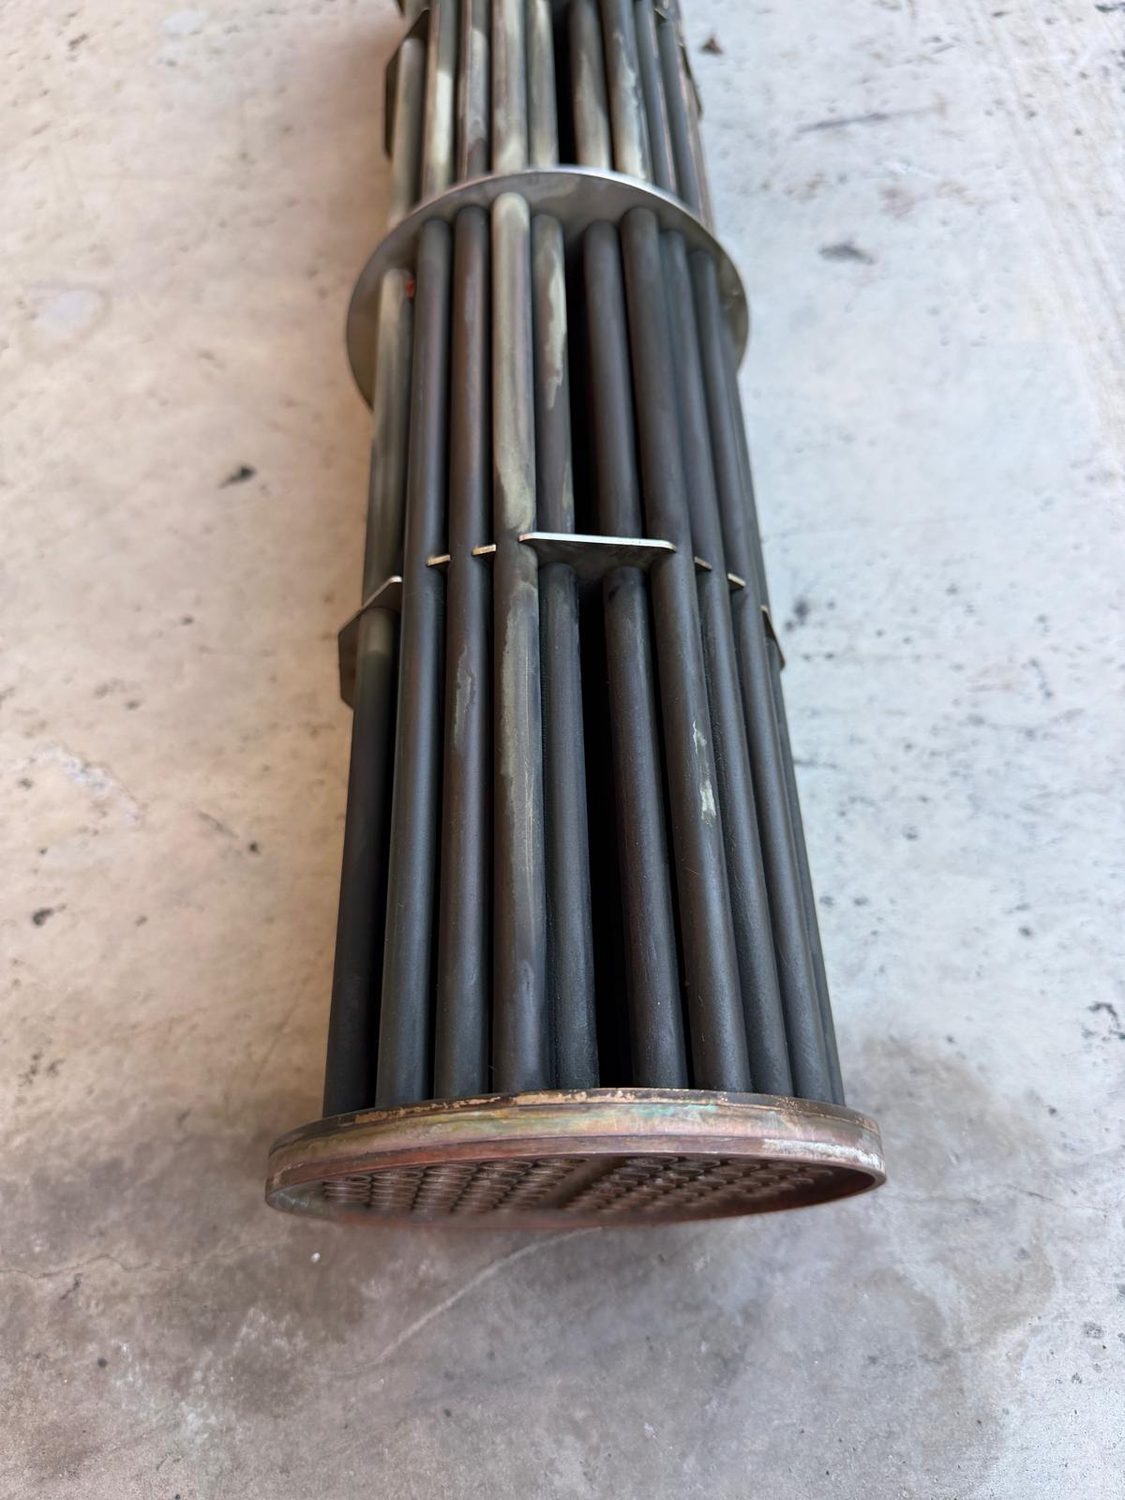
Tube-end bore at the flange face. Scale and oil sludge bridging the tube ends on the left; the same bore after the immersion cycle on the right. Drag the handle across to compare.
The results
Hardware and chemistry
Tanks and rod retrofits
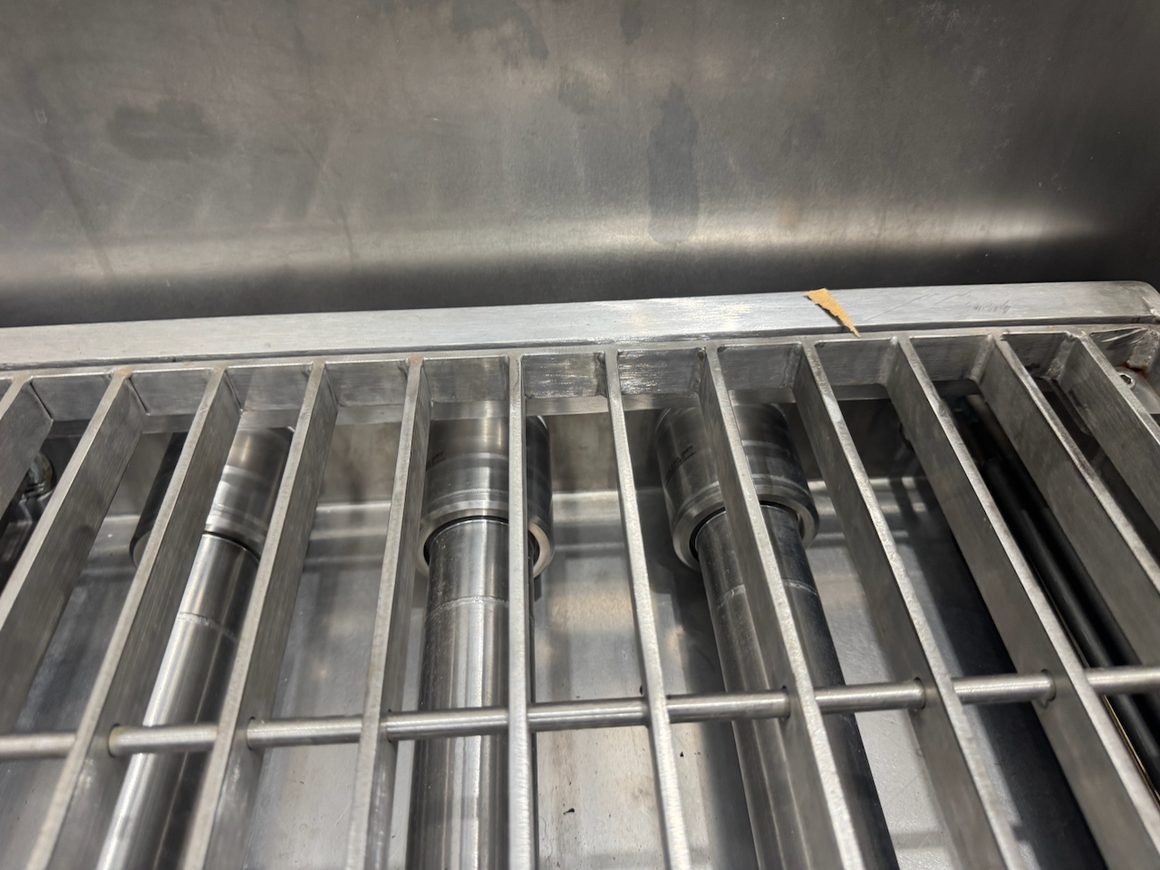
Industrial tanks for cores and radiators; 360° rod resonator sets convert existing bundle pits into live cleaning vessels.
Read the rod retrofit guide →
CoreKleen HX
The heat-exchanger degreasing grade, paired with inhibited Descale for waterside scale.
View the product, SDS and TDS →